Techno Multi Services
Reverse Osmosis (RO) Plant Manufacturer in Pune
Turnkey Industrial & Commercial Reverse Osmosis (RO) Plant Manufacturer in Pune
Industrial operations across Western Maharashtra’s manufacturing belts face acute groundwater mineral contamination. Deep borewell water in Chakan, Bhosari, Talegaon, and Ranjangaon frequently registers Total Dissolved Solids (TDS) levels between 1,500 and 4,000 ppm, accompanied by elevated levels of chlorides, sulfates, silica, and temporary bicarbonate hardness.
Feeding high-TDS, mineral-laden water directly into industrial boilers, chillers, cooling towers, or sensitive manufacturing processes results in severe consequences. Boiler heat exchanger tubes suffer rapid limescale crystallization; a mere 1.5mm layer of scale creates a 12% to 15% increase in fuel consumption and elevates the risk of catastrophic boiler tube ruptures. In electronic plating, automotive washing, and pharmaceutical formulation, high-mineral water causes spotting, coating defects, and product batch rejections.
However, poorly engineered industrial RO systems turn into maintenance nightmares. Without precise hydraulic flux modeling, effective antiscalant conditioning, and automated Clean-In-Place (CIP) architectures, thin-film composite (TFC) membranes suffer irreversible biofouling and silica scaling within months. Plants experience rapid permeate flow decay, frequent membrane burnouts, and skyrocketing operating expenses.
Engineered Solution & Technical Value Proposition
Techno Multi Services (TMS Water Solution) designs and manufactures heavy-duty industrial and commercial Reverse Osmosis (RO) plants engineered for maximum thermodynamic recovery and membrane longevity. Utilizing advanced hydraulic modeling software and premium spiral-wound polyamide composite membranes, our RO skids consistently deliver up to 80% water recovery with 99.2% to 99.6% salt rejection across the most demanding feed water profiles.
Brackish Water Industrial RO (BWRO)
Engineered for high-TDS groundwater (1,000 to 5,000 ppm TDS) utilizing high-surface-area brackish water membranes and energy-efficient SS316 vertical multistage pumps delivering pure process water.
Effluent & Wastewater Recycling RO (ETP/STP-RO)
Equipped with specialized Low-Fouling (FR) membranes with proprietary surface chemistry that resists organic adsorption, preceded by ultrafiltration (UF) pre-treatment for heavy-duty tertiary recycling.
Two-Pass / High-Purity RO Systems
Permeate from the first pass is routed through a second RO stage, stripping residual monovalent ions to deliver conductivity < 2.0 µS/cm for pharmaceutical, laboratory, and high-pressure boiler applications.
Industry Niche Applications Pune
Industrial Boiler Feed & Steam Generation
Demineralized RO permeate eliminating boiler tube scaling, reducing blowdown losses by 80%, and conserving substantial boiler fuel.
Chakan, Ranjangaon, Kurkumbh, Baramati
Automotive Paint Shops & Surface Finishing
Ultrapure rinse water (Conductivity < 10 µS/cm) preventing water-spotting and adhesion defects in electro-deposition (CED) paint lines.
Chakan, Talegaon, Bhosari
Pharmaceutical Formulation & Healthcare
Sanitary SS316L two-pass RO skids equipped with orbital-welded piping, providing purified water conforming to IP/USP pharmacopeial standards.
Kurkumbh, Hinjawadi, PCMC
Commercial Real Estate & IT Campuses
High-capacity commercial drinking water plants providing safe, crystal-clear drinking water across large IT corporate campuses.
Hinjawadi, Magarpatta, Kharadi, Viman Nagar
Engineering Specifications & Design Parameters
Parameter / Metric |
Inlet / Raw Water Standard |
TMS Guaranteed Outlet / Treated Standard |
|---|---|---|
|
Feed Water TDS Range
|
Up to 5,000 ppm (BWRO)
|
TDS < 20 – 50 ppm
|
|
Salt Rejection Efficiency
|
—
|
98.5% – 99.6%
|
|
Recovery Ratio
|
100% Raw Feed
|
65% – 85% Permeate
|
|
Turbidity (NTU)
|
< 5.0 NTU (Pre-filter)
|
< 0.1 NTU
|
|
Silt Density Index (SDI₁₅)
|
< 3.0 (Post-cartridge)
|
< 1.0
|
|
Product Water Hardness |
300 – 1,200 ppm
|
< 2.0 ppm (Near zero)
|
- Capacity Range - 500 LPH, 1,000 LPH, 2,000 LPH, 5,000 LPH, 10,000 LPH, 25,000 LPH to 100,000 LPH+
- Materials of Construction - SS304/SS316 structural skid frame, Schedule 80 UPVC / SS316 high-pressure piping, ASME-certified FRP pressure tubes.
- Automation & Instrumentation - PLC microprocessor panel with digital conductivity/TDS meters, pressure transmitters, low/high pressure cutoffs, and digital rotameters for permeate and reject streams.
6-Step Turnkey Project Delivery Workflow
- 01. Comprehensive Water Chemistry Analysis - Detailed lab testing analyzing TDS, Silica, Hardness, Iron, Chlorides, and calculation of Langelier Saturation Index (LSI).
- 02. ROSA / WAVE Membrane Projection Modeling - Computerized membrane simulation optimizing flux rate, staging ratio (e.g. 2:1 array), and recovery percentage without scaling risk.
- 03. Skid Engineering & Structural Fabrication - Modular SS304/SS316 skid fabrication, high-pressure piping manifold welding, and vibration-damped pump mounting.
- 04. Factory Hydrostatic & Quality Testing - 1.5x working pressure hydrostatic testing of all manifolds, seal integrity verification, and electrical panel megger testing.
- 05. Site Erection & Pre-Treatment Commissioning -On-site positioning, media loading, backwashing, antiscalant calibration, and high-pressure slow-pressurization startup.
- 06. Performance Guarantee Run & CIP Training - 72-hour continuous trial run logging flux and rejection parameters, followed by hands-on training for client operators on CIP chemical wash.
Frequently Asked Questions (High-Value Technical & Commercial Answers)
Capital cost depends on capacity, feed water TDS, and material specifications: a standard commercial 1,000 LPH RO plant typically ranges from ₹1.8 Lakhs to ₹3.2 Lakhs; a 5,000 LPH industrial skid costs approximately ₹5.5 Lakhs to ₹9.5 Lakhs; while large-scale 10,000 to 25,000 LPH automated SS316 plants range from ₹12 Lakhs to ₹28 Lakhs. High-purity pharmaceutical or wastewater recycling skids incur additional costs for specialized sanitary piping and ultrafiltration.
Under optimal pre-treatment and proper antiscalant dosing, an industrial RO plant requires Clean-In-Place (CIP) chemical cleaning every 3 to 6 months. CIP should be triggered immediately if you observe a 10–15% drop in permeate flow, a 10–15% increase in differential pressure, or a 5% increase in salt passage. TMS provides automated CIP systems that restore membrane performance within 4 hours.
Depending on your site requirements, RO reject water can be repurposed for toilet flushing, cooling tower makeup, dust suppression, or gardening (if TDS is below vegetative tolerance limits). For zero-discharge industrial applications, we integrate the RO reject into our high-recovery secondary RO stages or Multiple Effect Evaporator (MEE) ZLD systems.
Reverse osmosis membranes have microscopic pore channels that are vulnerable to abrasion and blockage by fine suspended particles. A dual-stage 5-micron and 1-micron sediment cartridge filter acts as an indispensable sacrificial barrier, stripping silt, pipe rust, and carbon fines to protect high-pressure pump impellers and prevent irreversible physical membrane fouling.
Yes, absolutely. When treated through our multi-barrier tertiary system (Pressure Sand Filter + Activated Carbon Filter + UV Disinfection + Chlorination), the water is completely clear, odorless, and microbiologically sanitized. It is 100% safe for dual-flush toilet cisterns, landscape horticulture, car washing, and HVAC cooling towers, saving millions of liters of fresh municipal water annually.
Yes. High silica (> 30–50 ppm) is common in Maharashtra basalt groundwater and creates rock-hard colloidal scale on membranes if untreated. We engineer specialized pre-treatment solutions using high-pH silica dispersant antiscalants, temperature conditioning, and recovery-stage management to safely operate with feed silica levels up to 120 ppm without scaling.
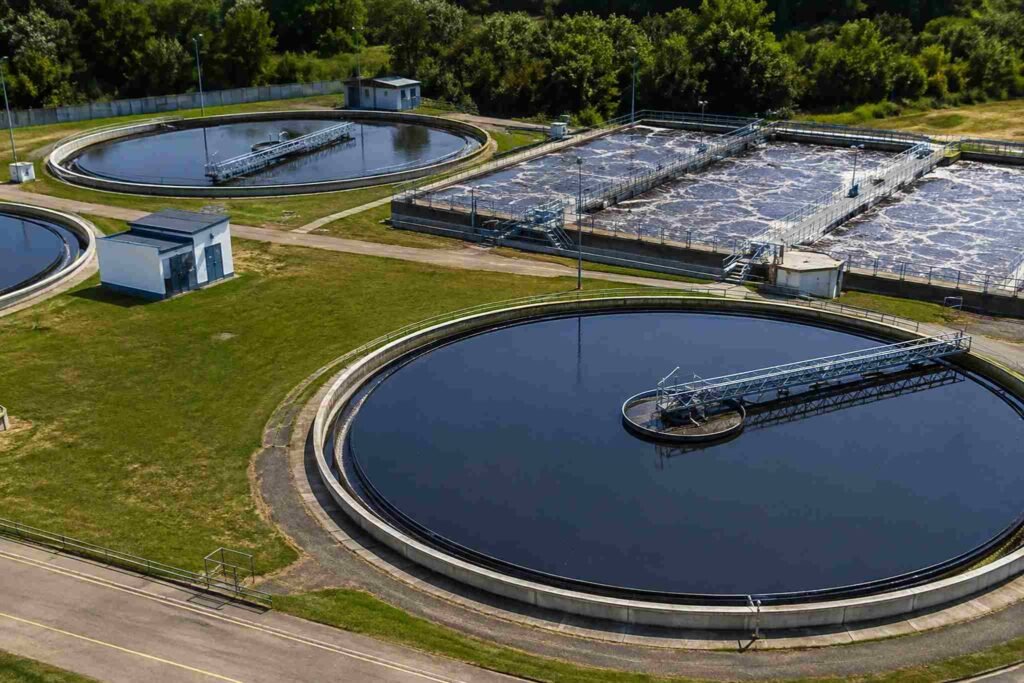
Our Other Treatment Services
Eliminate Boiler Scale & Get Ultrapure Water for Your Plant
Request a Free Water Analysis & Customized Membrane Projection Simulation (ROSA/WAVE).